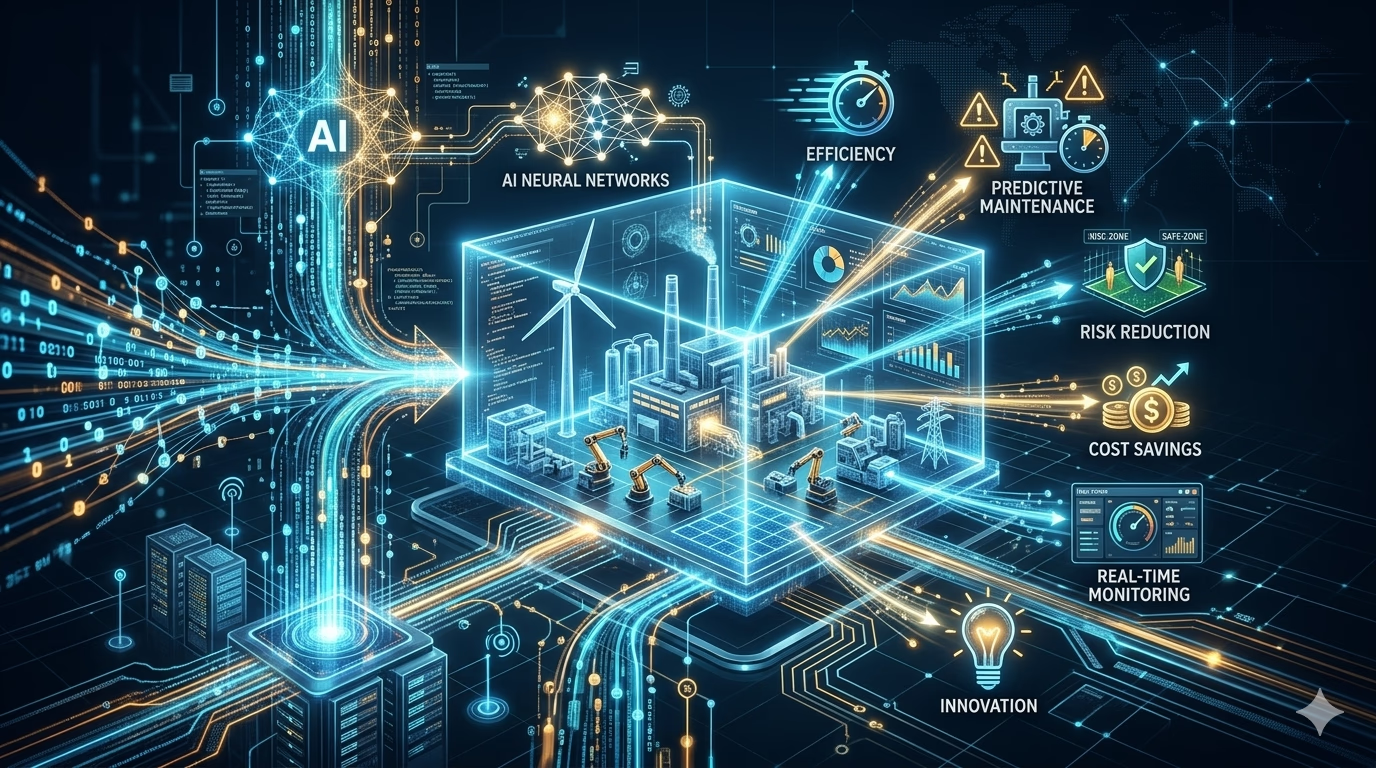
Digital twins enable continuous observation of production systems through synchronised sensor data. This lets manufacturers identify problems early and significantly reduce equipment downtime, keeping operations at peak efficiency.
Predictive maintenance is another key advantage: by monitoring machinery conditions continuously, businesses anticipate failures before they occur, avoid costly interruptions and extend equipment lifespan while improving overall performance.
The technology also promotes environmental responsibility by allowing simulation of resource consumption before implementation. Manufacturers can test strategies to lower energy use, minimise waste and reduce their footprint through virtual modelling rather than real-world trial and error.